Dies
Stamping, progressive and forming dies, built by qualified tool and die makers.
- Die types
- Progressive · compound · blanking · forming · draw · trim
- Built by
- Qualified tool and die makers
- Tool steel
- D2 (1.2379) · A2 · carbide inserts for long runs
- Hardness
- 58 – 62 HRC on cutting elements
Overview
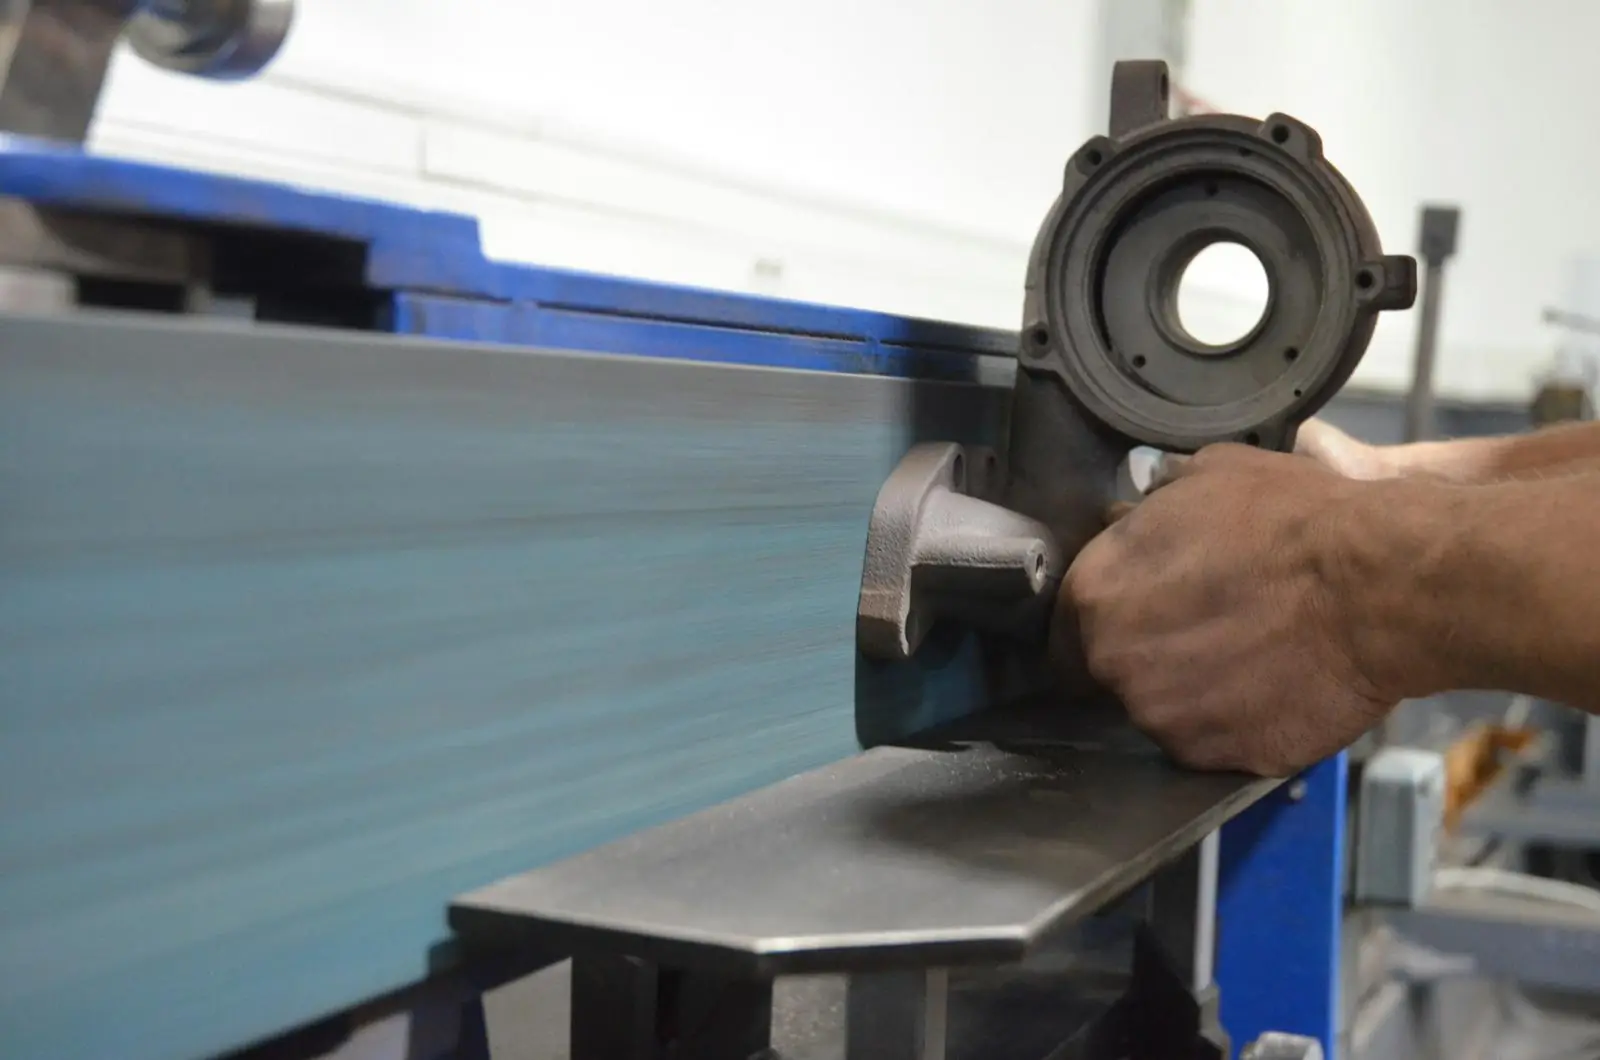
The group began as a die and tool maker in 1997, and dies remain at the core of what we do. Our qualified tool and die makers design, machine, heat treat, assemble and try out every die in-house, from single-stage blanking dies to multi-station progressive tools for high-volume production.
Our capabilities
- 01Progressive dies for high-volume stamping
- 02Compound and blanking dies
- 03Piercing, notching and trimming dies
- 04Forming, bending and draw dies
- 05Transfer and line dies
- 06Die tryout and first-article approval
- 07Spare punches, inserts and buttons
- 08Die maintenance, sharpening and rework
How a progressive die works
Each press stroke advances the strip one pitch while every station works at once: pierce, notch and finally blank the finished part. Our tool and die makers design the strip layout, build every station and prove the die in tryout.
Technical data
| Die types | Progressive · compound · blanking · forming · draw · trim |
|---|---|
| Built by | Qualified tool and die makers |
| Tool steel | D2 (1.2379) · A2 · carbide inserts for long runs |
| Hardness | 58 – 62 HRC on cutting elements |
| Design | Strip layout and 3D die design in-house |
| Tryout | Tryout and first-article parts before dispatch |
Values reflect common industry practice and referenced standards. Final values are set by your drawings and specification.
Our project approach
- 01
Submit drawings & specs
Send your drawings, specifications and quantities. DXF, DWG, STEP or PDF.
- 02
Proposal
A clear technical and commercial proposal with price, scope and delivery date.
- 03
Manufacturing
Fabrication, finishing and inspection to the agreed quality plan.
- 04
Shipping, delivery & local assembly
Delivered to your site, with assembly and installation support locally.
FAQs
What types of dies do you build?
Progressive dies, blanking and piercing dies, compound dies, forming and bending dies, and transformer lamination dies.
Which tool steels are used?
Cutting and forming sections are typically made from tool steels such as D2 or A2, hardened to around 58–62 HRC, with the grade chosen for the material and volume being pressed.
Who manufactures the parts?
Parts are manufactured within the Ferrokshar Group, in production since 1997. Engineering, project management and on-site support are handled by our team in Toronto, ON.
Who do I deal with?
Our engineering team is your single point of contact, from quote to delivery and after-sales service.
Request a quote
Send your drawings and specifications. Our engineers will reply with a detailed proposal.